Showing posts with label Pumps. Show all posts

Monday, 28 September 2026

Pump portal.

The launch of MyNETZSCH, a new digital customer portal has been launched by Netcsch Pumps & Systems, demonstrating its continued commitment to customer satisfaction.

With MyNETZSCH, the company is expanding its digital service offering with a central customer portal designed for operators, service managers, and purchasing professionals. The platform brings together key information and processes related to NETZSCH Pumps & Systems in one place, providing fast access to machine data, technical documentation, and spare parts ordering.

Through digital self-service features, MyNETZSCH helps companies streamline information and procurement processes while simplifying day-to-day service operations. Users benefit from location-independent, 24/7 access and a platform tailored to their individual requirements.


@netzschpumps @pressebox @UnnGmbh #Pauto

Thursday, 30 April 2026

Girls’Day 2026.

Discovering technology, opening perspectives.

As part of Girls’Day 2026 (22/4/2026), NETZSCH Pumpen & Systeme offered female students hands-on insights into technical fields of work and training. This German nationwide initiative aims to spark early interest in technical professions and highlight career paths beyond traditional role models.

At the Waldkraiburg site, the participants had the opportunity to get to know the company and experience various technical disciplines first-hand. From IT and development to design and production, they gained an impression of the wide range of technical career opportunities within an international mechanical engineering company.

For NETZSCH, Girls’Day is part of a long-term commitment to promoting diversity and young talent in technical professions. Further details on the program and the experiences of the participants can be found in the full article on the NETZSCH Pumps & Systems website here.


@netzschpumps @Der_GirlsDay @UnnGmbh @PresseBox #Pumps #Germany

Thursday, 12 March 2026

Four new intelligent pumps.

Four innovative diaphragm pump features for flow, pressure, and vacuum control as well as versatile dosing have been introduced by KNF. These solutions set a new benchmark for precision, reliability, and adaptability. These new intelligent liquid, gas and vacuum pumps feature integrated sensor technology offer advanced closed-loop control for achieving and maintaining flow, pressure or vacuum as well as precise dosages.

For liquid metering applications, KNF has developed the FMS-FC 1.400. This diaphragm pump with integrated Flow Control uses a precise flow sensor and ensures precise, accurate, and stable liquid delivery. It achieves a maximum flow rate of 3.4 l/min, a maximum pressure of 6 bar (rel.) and offers a maximum suction height of 3 mH2O.

Another intelligent liquid diaphragm pump innovation is the FD 1.200 with Versatile Dosing which delivers precise and repeatable volumes for demanding applications. For this, it uses advanced stepper motor technology and actively actuated valves. It offers a maximum flow rate of 40 ml/min, a maximum pressure of 6 bar (rel.), and a suction height of at least 4.5 mH₂O. Compact, chemically resistant, and customizable, it sets a new standard for accurate dosing.

The new MGP 75 diaphragm gas pump with intelligent Pressure Control maintains precise and consistent gas pressure even under changing conditions. Using the latest KNF motor technology, it achieves a maximum flow rate of 78 l/min, a maximum pressure of 1 bar (rel.), and a maximum vacuum down to 25 mbar (abs.).

Equipped with the intelligent feature Vacuum Control, the new micro vacuum pump NVC 830 maintains exact vacuum levels in demanding environments. This compact pump delivers a maximum flow rate of 4.7 l/min and a maximum vacuum down to 55 mbar (abs.). Intelligent features for maximum precision.
Each pump integrates modern sensor technology and proprietary motor control to maintain exact setpoints, even under dynamic conditions like changing pressure or media temperature. This integrated closed-loop control reduces engineering efforts to a minimum. It makes the potentially difficult integration of external sensor and development of new control logic from scratch obsolete.

Flexible connectivity and integration.
The pumps can operate autonomously or can be controlled via analog signals such as control voltage. For use in complex systems, the pumps also support modern communication protocols like UART, enabling seamless integration into smart environments.

Demanding applications.
Based on a modular design, the pumps can be customized quickly and cost-effectively. Options include material selection, electrical and line connections, and digital settings such as output setpoint, ramp-up speed or maximum motor speed limits, depending on the pump. This flexibility makes the pumps an ideal choice for critical applications in industries including medical technology, analytical systems, and industrial processes.


#KNF #PAuto @mepaxIntPR

Tuesday, 6 January 2026

Diaphragm pump leadership.

Diaphragm pump manufacturer KNF is beginning a new chapter in its leadership as Alexander Heizler takes over as CEO, following Martin Becker’s move to focus on his role as Chairman of the Board of Directors. He has been with the company since 2009 and served as Chief Operating Officer (COO) since 2021. His appointment ensures continuity and reflects KNF’s commitment to long-term stability as a family-owned business.

Alexander Heizler
“I am honored to take on the role of CEO,” says Heizler. “KNF stands for technological excellence, strong values, and a dedicated global team. I look forward to continuing this successful journey.”

After more than 40 years at KNF, including 26 as CEO, Martin Becker is stepping down from operational leadership. He will now fully focus on his role as Chairman of the Board of Directors, where he looks forward to continuing his close and trusted collaboration with Alexander Heizler in a new capacity. This marks the completion of a carefully planned transition. Martin Becker will also remain connected to the company as a shareholder.

“Passing on the operational leadership of KNF is a deeply personal step for me,” Becker explains. “I am proud of what we have built together and fully trust Alexander Heizler to lead the company with passion and responsibility.”

"This leadership change underscores KNF’s enduring values and its clear vision for the future as a global technology leader. With over 900 employees worldwide, KNF remains committed to innovation, sustainability, and customer-focused diaphragm pump solutions.""


#KNF #PAuto @mepaxIntPR


Wednesday, 27 November 2024

Micro vacuum pump.

The new MPXS series from COVAL offers one of the most compact intelligent vacuum pumps on the market, without compromising on the technologies that characterise the French brand. COVAL's aim is to provide manufacturers with an even more efficient tool for handling non-porous parts at high speeds on robots or automated systems.

The MPXS micro vacuum pump stays true to the design principles of COVAL's intelligent vacuum pumps, which are energy-efficiency, high-performance and communications I/O. It adds ultra-compactness, and thus concentrates all the qualities of COVAL's intelligent vacuum pumps into a smaller physical space.

With a width reduced to just 12.5 mm and a weight of only 87 grams, the MPXS micro vacuum pump is the smallest vacuum pump ever designed by COVAL. This size means it can be installed as close as possible to the suction cups, inside restricted spaces, for reduced pick-up time with no loss of load, guaranteeing high speeds.

MPXS series micro vacuum pumps quickly reach a maximum vacuum of 85%, thanks to single-stage Venturi technology, and is thus perfectly suited to dynamic applications requiring very short cycle times. The two power levels of 15 and 26 Nl/min add to their versatility and enable them to adapt optimally to the needs of each application.

The MPXS micro vacuum pump provides the user with useful information at every stage of operation. Its Human Machine Interface (HMI) makes it easy to read operating, diagnostic and maintenance information, and enables rapid parameter setting. Additionally, the integrated IO-Link communication interface supports fast, cost-effective installation, continuous diagnostics, centralized parameter setting and efficient communication with higher-level protocols (EtherNet/IP, PROFINET, EtherCAT...).

These micro vacuum pumps feature ASC (Air Saving Control) technology, which intelligently regulates vacuum generation, enabling energy savings of 90% on average by stopping air consumption once the desired vacuum level has been reached.

The modularity of the MPXS series offers a wide choice of configurations, ensuring great flexibility of installation and use to suit the varied needs of industrial applications. It is available as stand-alone modules, or in islands of up to 8 modules, with standard or powerful adjustable blower options. The MPXS series is precisely tailored to each application, for maximum efficiency.

The pump's small size, high performance and wide range of functions and configurations make it ideal for industrial applications requiring high speeds: High-speed pick-and-place, robot manipulators, automated production. Especially in use in the plastics, electronics and pharmaceutical industries.


@COVAL_SAS @mepaxIntPR #PAuto  

Wednesday, 27 March 2024

Metal-free pumps.

Electrophoresis with agarose gel is an important method for analysis and quality control in the life sciences. The basis for precise results is the accurate filling of the agarose columns. This process works with metal-free pumps from HNP Mikrosysteme GmbH.

Pumps from HNP Mikrosysteme are used for demanding filling tasks in various industrial sectors. One task is the production of agarose columns for electrophoresis applications. Here, a low-percentage agarose solution is filled into plastic capillaries at up to 65 °C in dosing quantities of 30 µl - 50 µl. The modular pump mzr-2942 is used. It is a metal-free pump. The wetted parts of this pump are made of ceramic and PEEK to prevent transfer of metal ions.

Agarose gels are used, for example, for the quality control of DNA and RNA samples after critical work steps during the production of genomic libraries. Sample volumes of only 2 µl - 5 µl are required. The results are available after just 20 to 30 minutes.

HNPM pumps ensure process reliability in applications where extremely small quantities of liquids are required. Five series of micro annular gear pumps (mzr-pumps) enable the smallest dosing volumes from 0.25 µl and volume flows from 1 µl/h to 1152 ml/min.


@PresseBox #HNPM #Pharma #LIfeScience

Tuesday, 12 December 2023

Pumps and systems appointment.

HNP Mikrosysteme has appointed of Suzanne Coleman Wilhelmsen as Head of Business Development for North America.

Suzanne Coleman Wilhelmsen
Prior to joining HNP Mikrosysteme, Suzanne invested herself and the majority of her career in the automotive industry, focusing her time and energy into companies including Audi of America and Audi AG in Ingolstadt, Germany, Volkswagen and Audi Financial Services (VW Credit), Lincoln (Ford) Motor Company, and Volvo Cars USA. Notably Suzanne managed the North American launch of the first generation Audi Q7, implemented many products and strategies to support these luxury automotive brands product growth and loyalty. Further, she played a critical role with Ford in successfully relaunching the Lincoln brand in the Great Lakes Region of the US. Her early career included an accomplished tenure in Change Management consulting with Accenture in the US and Europe.

“Suzanne brings deep OEM experience and extensive automotive product marketing know-how to our team. Her outstanding accomplishments in leading client experience initiatives, as well as her strong international business experience, is simply outstanding,” says Thomas Weisener, CEO of HNP Mikrosysteme.

In addition to living and working for many years in Germany, Suzanne has travelled extensively both internationally and nationally and is fluent in both German and English. Suzanne is a graduate of the University of Colorado Boulder where she earned her Bachelor of Fine Arts (BFA), after which she went on to earn her Post-Baccalaureate degree in Art Education from The School of the Art Institute of Chicago. Suzanne is an avid skier and certified professional ski instructor, who also worked for Vail Resorts in her formative years. She enjoys trail and endurance running, as well as hiking, backpacking, camping, and the arts - especially ceramics. Suzanne’s greatest accomplishment, however, is her role as Mom to three.

Yvonne Eilers, CFO of HNPM added, “Suzanne’s charisma and leadership in working with our sales teams has already made an immediate impact on our sales growth, and solicited glowing reviews from our clients. We are all excited to welcome her as a member of our leadership team. ”

Suzanne will be located in Chicago’s western suburb of Schaumburg, (IL USA)


@PresseBox #HNPM #Automotive #USA

Tuesday, 14 November 2023

Hydraulic motor is 95% efficient.

The H1F fixed displacement bent axis hydraulic motor has been launched by Danfoss POwer Solutions. Designed for open- and closed-circuit applications, the H1F motor offers best-in-class efficiency, proven reliability, and a compact design.

The latest development in Danfoss’ high-power H1 series of pumps and motors, the H1F fixed bent axis motor offers overall efficiency of up to 95%. High-efficiency motors deliver fuel savings, improve productivity, and reduce heat generation. Together with its high pressure and speed ratings, the motor enables operators to maximize the performance of their machines.

The new H1F motor builds upon the capabilities of Danfoss’ field-proven H1B variable displacement bent axis motor. The H1F motor uses the same high-quality nine-piston H1B rotating group and optimized single-piece flange, delivering long-lasting reliability.

The lightweight H1F motor features a power-dense, compact envelope for ease of installation. With its short length and 32-degree angle, the package size is one of the most compact on the market, enabling machine manufacturers to reduce the space claim of the hydraulic system.

“H1F represents the continued evolution of the H1 series, our popular, customer-trusted line of high-power pumps and motors. While this is a new motor for Danfoss, it is leveraging a design that has been on the market for over 10 years with more than 1 million rotating kits in use,” said Kenneth Befus, portfolio manager, Hydrostatics, Danfoss Power Solutions. “In our H1F motor, OEMs and distributors will find high quality, proven technology, market-leading efficiency, and outstanding speed and pressure performance.”

The H1F fixed bent axis motor is designed for closed- and open-circuit applications in agriculture, construction, and forestry machinery. It is ideal for fan drives, feeder drives, drill drives, track drives, winches, and vibration and shaking functions. The motors will be available in SAE, DIN, and cartridge flange styles, with twin, side, and axial port configurations. Integrated loop flushing and speed sensing are options; future additions will include a bolt-on counterbalance valve and load-holding valve for open-circuit applications. The first frame size, 80cc, is now available. Additional sizes will follow, ranging from 60cc to 250cc.


@DanfossPower @Danfoss @NapierPR #Automation #PAuto

Tuesday, 18 April 2023

Fan, pump and compressor drive.

Delta's Open-Loop Variable Torque Standard Drive VP3000 for fan, pump and compressor applications has just been launched. Itis specially designed to enhance fluid machine operation efficiency and reduce inverter harmonic distortion for a wide range of fluid applications. The VP3000 series offers excellent performance and stability with support for high-efficiency motors including induction motors, permanent magnet motors, and synchronous reluctance motors from 0.75 to 630kW. The new drive will be among the highlights at the Delta booth at Hannover Messe 2023 (Hall 11, Stand C20).

“For fluid machine operation, the customers are now looking for high efficiency to reduce energy and CO2, lowered harmonic distortion and user friendly functions. By offering greater power density of 23% lower cabinet volume on average, and low harmonic distortion of down to THDi 35%, the VP3000 is able to satisfy regulations across Europe, the Middle East, and Asia,” said Landers Yeh, Product Manager, Industrial Automation Business Group, Delta Electronics EMEA region. “We’re confident this new variable-torque drive is going to be very competitive.”

Highest Standard and Low Harmonic Distortion.
The new VP3000 drives from Delta come with an array of integrated safety features. Safe torque off (STO) SIL3, the highest safety integrity level that applies to machine systems. Built-in EMC filters provide electromagnetic compatibility up to C2/C3. The drive is resistant to moisture and dust with coating 3C3. By using film cap topology to replace traditional electrolytic capacitors, Delta was also able to lower the drive’s harmonic distortion down to 35%, far below the EN 61000-3-2 standard which specifies a total harmonic distortion (THDi) of less than 48%.

Energy-saving and User Friendly Functions.
Compared to the general motor drive, the higher power density of the VP3000 allows for a 23% lower cabinet volume on average. In some cases, the volume of the unit can be decreased by as much as 55%. The high-power models can also mount durable and easy-to-maintain floor-type modules, which increase space utilization and simplify assembly for easier and faster operation. It also helps improve motor productivity and efficiency, reducing carbon emissions for environmental sustainability as a critical part of device-based energy saving.

Equipment in the heating, ventilation, and air conditioning industry as well as water treatment facilities will benefit from the drive’s advanced features, which enable the movement of fluids using fans and pumps. The new drive also has a predictive maintenance feature for key components, which helps users pre-schedule service to ensure the stable operation of machines.

@mepaxIntPR #deltaww #PAuto #HM23

Monday, 7 November 2022

"Talking the torque in test rigs?"

To analyse the long term performance and reliability of hard working valves and pumps, serial innovators Manchester-based Bifold Group (GB) has adopted digital torque transducers from Sensor Technology Ltd for two of its specialist test rigs.

An inter-generational commitment to advancing science and engineering has seen Bifold transform from a 19th century mining lamp maker into a leading manufacturer of instrument valves and accessories, piping valves and pumps for the oil, gas and wider industrial markets. It has particular expertise in subsea and wellhead control systems and has also developed market leading technology in areas such as solenoid valves with ultra-low power requirements.

Its corporate development is just as impressive as its technical advancements. Over the last 10-15 years it has consistently grown profits by 50% a year, and is on course to clear £33m this year. During this period it has moved into bespoke premises, created about 250 high value jobs, developed new products and technologies and entered high tech markets around the world. Today 95% of its output is exported.

By using the power of computer aided design many of Bifold’s products are built to custom designs, yet they are produced to very short lead times thanks to the efficiency of internet communications. To maintain this standard, sample products and components are comprehensively tested so that their reliability and capabilities are never in doubt. Bifold is as innovative in developing its test regimes as it is in advancing its product technologies and business systems. So when it wanted to assess the effects of wear on its long-life valves it set about designing a special test rig. 

Engineer Andrew Laverick recalls: “We wanted to measure the power required to operate the valve to see how it changed over time and with long term use. It was clear that the best way to do this was to measure the torque input over an extended period. We were open to any design concept for the test rig, but soon found ourselves gravitating towards a TorqSense solution because the Sensor Technology engineers were so helpful and really knowledgeable about test rigs.”

Sensor Technology’s Mark Ingham explains: “TorqSense has been used on many test rigs over the years and I was delighted to hear the Bifold engineers say how easy it is to use and how robust the software is.”

Laverick again: “As a test engineer you are almost resigned to long set up procedures and software that falls over at the drop of a hat. But Sensor Technology has designed these problems out of their TorqSense equipment, with the result that we were able to complete our long term test procedures with the minimum amount of fuss and heartache and well within the allotted time schedule.”

In fact Bifold has since bought a second TorqSense which is being fitted to a new test rig used to assess the performance of mission critical chemical injection pumps, as used at oil and gas wellheads and on process pipelines.

“This project is proceeding well,” says Laverick, “and is allowing us to further develop our abilities to quickly provide bespoke equipment for ultra demanding applications, safe in the knowledge that it will perform faultlessly over a long working life.”

@sensortech  #PAuto #Torque

Wednesday, 5 October 2022

Motor or pump vibration trips.

Excessive vibration in a motor/pump is symptomatic of a problem that can cause further damage or deterioration. If ignored, the results are higher maintenance and downtime. In some situations, it could also lead to safety concerns.
Vibration sensors or accelerometers can be installed to detect abnormal vibration levels. Alarm trips can monitor the vibration sensors and provide a local trip source for the motor. These pumps can be installed in many different environments so Class I, Div 2/Zone 2 certification and wide ambient temperature specs for these alarm trips are key characteristics.

If necessary, the vibration levels can also be retransmitted back to the control system using the Analog Output signals from the alarm trips.

The Moore STA Functional Safety Limit Alarm Trip logic solver is shown in the diagram which is IEC61508 certified. If the loop isn’t part of a safety instrumented system (SIS) where a standard alarm trip will do, then their SPA2 Programmable Limit Alarm Trip would be a great alarm trip choice.

@MII_Worldwide #Automation #Pumps

Friday, 20 May 2022

Predictive maintenance for rotary equipment.

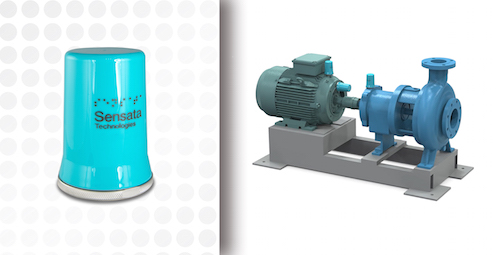
A new asset monitoring solution that enables predictive maintenance for rotary assets and delivers actionable insights to plant managers has been launched by Sensata Technologies.

Unplanned downtime related to motors, pumps, and other rotating assets costs plants millions of dollars in production every year. But existing solutions do not provide the real-time insights plant managers need to truly monitor their assets.

The new wireless 6VW series IoT sensor delivers insights via the Sensata IQ platform and can simultaneously monitor each asset using six sensing modalities - vibration, temperature, acoustic emission, speed, humidity, and magnetic flux. The sensors are designed for easy retrofit into a wide range of existing rotary assets - such as motors, pumps, blowers, fans, or compressors - regardless of brand or manufacturer with no changes needed to the company’s hardware or control platforms. The 6VW sensor series is an easy-to-use, self-install solution with a mobile app for device configuration, making setup and installation possible in less than five minutes.

Using powerful AI-driven algorithms explicitly designed for rotary assets by Nanoprecise, a Sensata technology partner, data from the sensor is analyzed at the edge for anomalies and then pushed to the Sensata IQ cloud-based platform for further analysis and data visualization.

The Sensata IQ platform uses the data to identify potential faults, calculate the asset’s projected remaining useful life and deliver alerts to plant managers on their laptops, tablets, or smartphones. The deep predictive maintenance analysis capabilities help plant managers rely less on manual walkarounds and better understand the health of their assets.

“The partnership with Sensata Technologies has been a tremendous success for both parties,” says Sunil Vedula, Founder and CEO of Nanoprecise. “Together, we know that our AI-powered solutions will help change the way plant managers around the globe monitor their rotary assets.”

Sensata is collaborating with technology companies such as Nanoprecise to develop comprehensive solutions for assets that are rarely monitored due to cost and complexity. Adding Nanoprecise’s technology to the Sensata IQ platform enables maintenance teams to make confident decisions and simplify maintenance programs across rotary assets with data that can be trusted and accessed anywhere, anytime.

“Sensata IQ is raising the bar in monitoring industrial assets, with reliable solutions that enable operators to easily increase productivity. This intuitive predictive maintenance solution, powered by Nanoprecise, allows plant operators to gain deep machine health insights on rotary assets in a simple way. Our mission is to make asset monitoring more accessible and this solution supports that mission.” says Naoto Mizuta, Vice President of Industrial at Sensata Technologies.

@Sensata #PAuto #AssetManagement

Monday, 20 December 2021

VFD manufacturer drives ahead!

Invertek Drives is expanding following significant growth in global sales.said the investment will create an expansion to its global variable frequency drive (VFD) manufacturing and distribution centre, along with the development of a new Application Centre.

It will create 85 new jobs over the next 12 months on top of the 280 people already employed at the global HQ in Mid Wales and follows a major recruitment drive over the past year in both its production and research and development departments.

The company designs and manufacturers VFDs used for the accurate control of electric motors used in many applications and industries globally. These range from conveyors to CNC machines, HVAC and ventilation systems, to water pumping applications

The VFDs are also major contributors to creating energy savings and reducing associated CO2 emissions in processes by making electric motors more efficient, cutting energy use by between 30% and 50% in many cases. They control the speed of motors, pumps and fans, ensuring they operate at optimum speeds.

They control the speed of motors, pumps and fans, ensuring they operate at optimum speeds.

Shaun Dean, CEO of Invertek Drives, and who is also Senior Vice President of Sumitomo Heavy Industries and CEO of Power Transmission and Controls Group (EMEIA Business HQ), said: “We’ve seen significant growth in sales and turnover over the past 18 months despite the global pandemic.

“Invertek’s approach to maintaining strategic stock of components has ensured we’ve been able to continue manufacturing our Optidrive range of VFDs despite the global supply chain problems currently facing many manufacturers.

“We continues to commit to investing heavily in the innovation, development and manufacturing of VFD technology. The expanded manufacturing facility will allow us to increase production from 350,000 units a year to 600,000.

“This is part of our drive to create the leading next generation VFD technology that will help to further reduce energy use and associated CO2 emissions globally.

We will add three new production lines each consisting of six Global Assembly Cells (GACS) allowing the increase in production."

Around eight billion electric motors consume nearly 50 per cent of the electricity produced in Europe. Globally, 40 per cent of electricity is used to power industry, with two-thirds of this used by electric motors. And yet less than 20 per cent of electric motors are controlled by VFDs.

@Invertek_Drives #Wales #Pauto #HVAC

Wednesday, 6 October 2021

Mini vacuum pumps.

Coval´s new LEMAX IO series of mini vacuum pumps with IO LINK communication integrate all the required functions for optimized vacuum management in a compact package. Via their IO-Link communications interface, the mini vacuum pumps communicate permanently with the environment and thanks to ASC (Air Saving Control) technology, combine productivity with energy savings, adapting to a multitude of applications in packaging, robotics or plastics processing. Without needing extra peripherals, these all-in-one mini pumps are fully compatible with Industry 4.0 automation.

IO-Link, simplified communication
The IO-Link interface ensures efficient real-time communication between LEMAX IO vacuum pumps and all the higher-level protocols (Ethernet/IP, PROFINET, EtherCAT, etc.) used for supervising the production line. IO-Link enables continuous diagnostics, centralized programming and pump control. The availability of real-time diagnostic status data makes it possible to optimize production. In addition to fast and cost-effective installation, preventive maintenance is easier and the replacement of vacuum pumps does not require reconfiguration.

Energy savings
ASC technology, which ensures intelligent vacuum control by stopping air consumption when the set vacuum level is reached, generates energy savings of between 75 and 99% depending on the application. In addition, ASC analyses the application and adapts to either impermeable or porous parts to optimize operation and energy consumption.

Compact size and light weight
Compact in size, the LEMAX IO pumps have all the principal functions integrated in a single module: pressure regulation, solenoid valves, anti-clogging open silencer, electronic vacuum switch, M8 connector (direct Plug & Play connection) and adjustable blowing. Their reduced size and weight (130 g) allow the suction cups to be positioned at minimum distance to achieve the shortest possible grip time without load loss.

Modularity
The LEMAX IO can be adjusted to the needs of integrators and users. They are available in three nozzle diameters (1, 1.2, 1.4 mm) allowing a suction flow rate from 29 to 70 Nl/min (max. vacuum 85%). They are optionally equipped with a normally closed (NC) or normally open (NO) solenoid valve. This variant is recommended for applications where gripping the workpiece must be guaranteed in case of an unexpected power failure, or even if leakage occurs (positive safety).

Several LEMAX IOs can be combined in an island with a single pressure supply.

@COVAL_SAS @mepaxIntPR #PAuto #Industry4

Wednesday, 27 January 2021

Chemical feed skid system.

Blue-White's CHEM-FEED® Engineered Skid Systems are now shipping! 

These Skid Systems are simple to operate, easy to order, and includes everything needed for precise chemical feed. The Triplex Skid allows for a two-pump injection system, with one pump acting as a backup to eliminate downtime and reduce costs in critical applications.

They ensure no leaky plumbing causing hazardous work environments with leak free threadless connections.

Blue-White's® lightweight, chemical and UV resistant, polyethylene, triplex skids ship fully assembled to save installation time, includes a built-in drip container, wall/floor mounting brackets, and a visual flow indicator.

It is recommended that these CHEM-FEED Skid System be equipped with their Proseries® Peristaltic Dosing Pumps.

There is a short 2-week lead time for this system.


@BlueWhiteInd #Pauto #Pharma

Friday, 13 November 2020

Long life disc pumps.

As part of its exclusive agreement with TTP Ventus to distribute the award-winning Disc Pump,  ION Science has introduced the long-life LT Series. These latest pumps offer in excess of 5,000 hours continuous operation under the most demanding conditions, with the potential to run up to 10,000 hours for other applications.

The LT Series is designed for applications with demanding operational life requirements. An excellent fit with ION Science’s photoionisation detection (PID) sensors, the new LT-S2-023 and LT-P2-024 models have higher power ratings than other models and deliver high performance without compromising on service life.

All Disc Pumps offer key features for  gas detection, monitoring, analysis and sampling industries including silent, vibration-free operation, true pulsation-free flow, fast response to set-point changes, high precision controllability and resistant to magnetic fields. 

These benefit many applications by allowing, simpler instrument design – especially for chromatographic systems, lower limits of detection, real time capability to respond to trigger conditions, intermittent sampling against pressurised lines, and improved user experience in wearable applications. 

Tom Harrison, Business Development Manager at TTP Ventus comments: “Over the first twelve months of our partnership, Ion Science has helped TTP Ventus to establish our presence the global gas detection industry. We’re now delighted to expand the range of pumps we offer to include the new LT Series. These long-life models take advantage of innovative design improvements that allow our pumps to be driven harder, for longer. The resulting performance boost broadens the number of applications that can take advantage of the core benefits of the Disc Pump platform, including fixed systems with long service intervals.”

Most piezoelectric gas pumps rely on the movement of a piezo actuator to compress the gas in a cavity which increases its pressure. Such ‘displacement’ pumps have limited performance because the movement of piezo actuators is very small. 

In contrast, Disc Pump’s piezo oscillates at ultrasonic frequencies to create an internal standing wave which enables much greater pressure and flow than traditional piezo pumps.

Turning an ultrasonic standing wave into useful pumped flow requires a highly specialised valve, able to respond in a matter of microseconds. The patent-protected Disc PumpTM achieves this delivering unrivalled pneumatic performance.  Disc PumpTM is already widely used in the gas and leak detection markets and the arrival of the LT series will open more applications.

@ionscience @ttpventus @elhcomms #Pauto #Environment

Friday, 15 May 2020

Drive Intelligence for servo pumps.

The new V2+ software for servo pumps that integrates directly into the drive, Baumüller enables greater process reliability and improved process quality, for example on pressing and injection mold machines

The servo pump solution is an intelligent and energy-efficient drive system e.g. for presses and injection mold machines. With the new V2+ software package, the company now offers more intelligent functions for process monitoring and process optimization. Thanks to years of intensive collaboration with mechanical engineers, Baumüller is able with its serve pump solution to significantly reduce the energy requirements of machines and systems, enabling relatively short cycle times with very low noise development and a high level of process precision. The combination of hydraulic power transmission together with the electric servo drive technology offer many advantages. The servo drive can optionally be adjusted for significantly optimized overall system effectiveness as compared to a purely hydraulic solution and for greater energy efficiency. Other positive secondary effects include improved process performance and low heat development.

Process reliability and process optimization with new V2+ servo pump software
The controller-integrated servo pump software is now available in a new, expanded version. The new software package for V2+ servo pumps offers new features especially in the areas of process monitoring, process optimization and process reliability.

With the feature for speed monitoring and slip speed compensation, service can now be planned: The leakage characteristic of the system is monitored, initiated by the machine controller. The speed is automatically readjusted as needed so that the machine continues running in the optimal range. If the leakage increases as the pump ages and a measurement value outside the tolerance is detected, the system returns an error message. The operator is thus informed automatically, enabling a pump change at the right time, which prevents downtimes and improves process quality.

Pressure sensor monitoring is another new feature that ensures process quality and prevents downtimes. As pressure sensors age, they become less accurate, so the sensor values are first optimized and then a sensor change will be indicated as inaccuracy increases. Pressure sensors also typically have a tendency towards zero drift, i.e. they indicate that there is pressure in the system when this is not the case. Pulsating alternating pressures arising in the servo pump system can cause damage to the pump. In this case, the converter would receive the incorrect information that pressure still needs to be reduced and would rotate the motor in the wrong direction. With the pressure sensor monitoring software feature, such a false response is avoided, thus preventing damage to the pump.

Many processes that use servo pumps require long pressure hold times, e.g. with injection molding machines when the shape has to be maintained. This increases the risk of a thermal overload and thus early pump wear and tear. With the temperature model in the V2+ servo pump software, the thermal pump load is calculated from speed and pressure. Upon reaching a critical threshold value, a bypass valve can be connected, for example, to prevent overheating.

The V2+ software version also includes the acceleration limitation function. This ensures a soft yet highly dynamic control mode and thus minimizes wear and tear on the machine.

The intelligent control algorithm for adjusting to different rates of increasing pressure was already integrated with the previous software version. With this feature, parameterization only has to be set once and the adjustment occurs automatically. The software enables an overshoot-free pressure jump in minimum time, thus ensuring an optimized process sequence.

These servo pump features are integrated directly into the controller as an order option and are available on the servo controllers of the b maXX 3300 family and on the mono units and the side-by-side system of the b maXX 5000 family.

#PAuto @be_in_motion @BM_Services @PresseBox

Wednesday, 4 September 2019

Distribution of disc pump agreement.

ION Science has confirmed an exclusive agreement with TTP Ventus to distribute its award-winning Disc Pump™ to the global gas detection market. The micropump platform offers a wide range of innovative features designed to deliver ultrafast millisecond response and more sensitive detection of gases including volatile organic compounds (VOCs).

An excellent fit with Ion Science’s market-leading photoionisation detection sensors (PIDs), the lightweight TTP Ventus piezoelectric pump offers key features for the gas detection, monitoring, analysis and sampling industries including silent, vibration-free operation, exceptional pressure and flow, true pulsation-free flow, fast response to set-point changes, high precision controllability and resistant to magnetic fields.

These benefit many applications by allowing, simpler instrument design – especially for chromatographic systems, lower limits of detection, real time capability to respond to trigger conditions, intermittent sampling against pressurised lines, and improved user experience in wearable applications.

The agreement between the two Cambridgeshire-based hi-tech businesses covers two Disc Pump product lines: the XP Series provides a combination of performance and efficiency benefits with a wide temperature range from -25 up to 55°C for supporting the most demanding applications whilst the BL Series is a lower cost, entry-level version.

Tom Harrison, Business Development Manager at TTP Ventus comments: “We are excited to partner with Ion Science to offer our Disc Pump to the global gas detection industry. It represents an opportunity to accelerate our growth in this previously untapped market by leveraging Ion Science’s extensive experience, worldwide presence and technological expertise.”

Duncan Johns, Managing Director at Ion Science adds: “The TTP Ventus Disc Pump is truly revolutionary making it an excellent fit with our well proven MiniPID sensor technology. Offering these complementary products under one roof helps us to respond to the ever increasing demand for rapid, sensitive detection of VOCs. We are confident the relationship will be a success and look forward to it further strengthening our position in the global gas detection market.”

The TTP Ventus Disc Pump is already widely used across a range of markets including medical, life science, environmental and defence. It offers two pumping chambers which are configured at the point of manufacture either in series for high pressure applications, or parallel for higher flow.

Most piezoelectric gas pumps rely on the movement of piezo actuator to compress the gas in a cavity which increases its pressure. Such ‘displacement’ pumps have limited performance because the movement of piezo actuators is very small.

By instead creating a standing wave TTP Ventus is able to deliver much greater pressure and flow than traditional piezo pumps. Further, Disc Pump operates at ultrasonic frequencies making it completely silent.

Turning an ultrasound standing wave into useful pumped flow requires a highly specialised valve, able to respond in a matter of microseconds. The patent-protected Disc Pump achieves this delivering unrivalled pneumatic performance.

@ionscience @ionscienceusa @elhcomms

Thursday, 9 May 2019

Pulsating free dispensing.

In the production of electric motors - more precisely in the casting of the coil in the stator - very liquid, low-viscosity materials are processed. A continuous pulsation-free dispensing flow of the material is particularly important here.

By trickling or impregnating the rotating drive components, the coils are provided with a protective layer. This process later improves the performance of the motors and generally extends their service life. After curing, the applied resin becomes a hard-elastic moulding material. It retains its good mechanical and electrical properties even at high temperatures. It insulates, prevents vibrations and the coils become more robust.

In order for the resin masses to harden, they - and also the stators - must be heated. This requires perfect process reliability. The components are either charged with electricity (electricity heat / induction) or heated in special industrial furnaces (circulating air heat) in so-called impregnation machines or trickle systems. The aim is a perfect trickle result and a precise flow of the resins between the windings of the coil.

ViscoTec dispensing systems are excellently suited for the application of resin masses. They can easily be integrated into existing production lines. However, they are also impressive in newly designed customer-specific systems.

The endless piston principle used in the ViscoTec dispensing pumps enables pulsation-free, continuous dispensing. Continuously adjustable in application quantity and application speed. Therefore, the dispensing technology specialist can guarantee an ideal penetration behaviour and a completely clean impregnation result, both when processing 1- and 2-component resin masses or trickle resins. ViscoTec dispensing pumps function regardless of viscosity. Even if viscosity fluctuations occur due to storage time or storage temperature, the dispensing functions perfectly. Dispensing is carried out from a dispensing tip with hose. A hardening of the pump is conceptually prevented.

The dispensing pumps are combined with the ViscoTec treating systems ViscoTreat-R or ViscoTreat-Inline. Thanks to optional vacuum suction, they ensure a completely air-free supply to the 1- and 2-component dispensers. The operator has no contact with the material.

Trickling is impressive in many respects: Precise dispensing results in specific material consumption per component. This ensures optimum impregnation. Constant and automatic processes are created. In addition, the resin is perfectly distributed on the coils. This in turn means reliable electrical insulation and improved thermal conductivity.

@ViscoTec #PAuto #Pumps

Monday, 21 January 2019

Cavitation detection.

Yokogawa has developed a cavitation detection system and will be available next month (Feb 2019). By detecting cavitation, quantifying information, and displaying the data in real time, this system provides an early indication of conditions that can result in a degradation in pump performance. By detecting problems early, before damage occurs which can cause an increase in both vibration and noise levels, this solution improves the efficiency of plant maintenance.

Components of Cavitation
Inspection System
Directed at sectors such as oil, petrochemicals, chemicals, iron and steel, pulp and paper, water supply and wastewater treatment, pharmaceuticals, food, etc., it will aid maintenance of plant facilities such as pumps that tend to deteriorate due to cavitation.

Cavitation in fluids can cause damage to pumps. To minimise this damage, it is necessary to detect cavitation at an early stage and take corrective measures such as adjusting the flow rate. One issue, however, is that there has been no way to quantify cavitation. In addition, since cavitation occurs inside equipment, it is impossible to visually check whether this is occurring. Cavitation is usually detected by field personnel who rely on experience gained on the job to detect changes in vibration and noise levels that are caused by excessive cavitation. However, even highly experienced plant personnel and specialists can miss these early signs, and such problems may go undetected until the inevitable increase in vibration and noise occurs.

In its analysis of this problem, Yokogawa has focused on the principle that there is a direct relationship between differential pressure and cavitation, and has created a condition monitoring solution that involves the quantification of cavitation based on pressure data.

The new product features:
1. Real-time detection -  The system that Yokogawa has developed consists of a STARDOMTM FCN-500 network-based control system, a Yokogawa cavitation detection logic program, and a highly accurate (±0.075%) DPharp EJX110A differential pressure transmitter, and relies on the FOUNDATIONTM Fieldbus industrial digital communication standard to link these components. At 100 ms intervals, the DPharp transmitter measures the pressure inside the target equipment, and this data is transmitted via the fieldbus network to the STARDOM FCN-500 system for processing in real time by the logic program. This system is therefore able to detect cavitation issues early on, allowing field personnel to take quick remedial action by, for example, reducing the flow rate to a level that suppresses cavitation without interfering with production line operations.

2. Troubleshooting - Valves, pumps, and other types of plant equipment can all experience problems such as cavitation which are caused by anything from the opening/closing of a valve, a change in viscosity level or some other physical property of a liquid, or a change in the external environment. Field personnel have traditionally relied on their own experiences and the use of analytical tools to find out what is causing these problems. Thanks to the development of this new system, field personnel will now have a tool that will help them troubleshoot problems with greater efficiency by identifying and quantifying cavitation in plant equipment.


@YokogawaIA #PAuto #Water